If you’ve ever walked the floor of a machine shop, a steel fabrication yard, or a metalworking shop, you’ve probably heard the high, whirring ring of a semi-automatic band saw long before you see the machine itself. As a semi-automatic band saw supplier, I talk to dozens of operators, fabricators, and shop managers every week, and more often than not, one question comes up consistently: “What’s the right feed rate for this thing?” It sounds like a simple question on the surface, but if you dig into how feed rate works, and how it changes from job to job, it’s actually one of the most critical variables that separates a smooth, low-waste cut from a rushed, inaccurate, or dangerous one. Semi-Automatic Band Saw
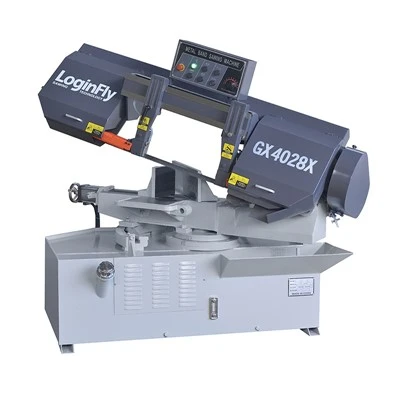
Let’s start with the basics for anyone who’s new to band sawing, or who’s only used automatic or manual models in the past. A semi-automatic band saw is, at its core, a middle ground: you load the material into the vise, activate the cycle to lower the blade and make the cut, and the machine stops automatically when the cut is done—no holding the feed lever by hand, no stopping early if your arm gets tired. That semi-automatic design is a big reason it’s so popular for small to medium job shops, prototype work, and production runs of 10 to 1,000 parts; it’s more consistent than manual sawing, more flexible than a full automatic that’s locked into a set blade size and material type. But that semi-automatic design also means the feed rate (the speed at which the blade advances through the material, measured in inches per minute, or IPM, or sometimes millimeters per minute) isn’t just a number you plug in and forget—it’s tied to three things: the material you’re cutting, the blade you’re using, and the result you need from the cut.
Most first-time operators look at the band saw’s control panel and see a feed rate dial that goes from 1 to 10, or 0 to 100, and assume higher is better. After all, faster cuts mean more parts per hour, less time tied up on the machine, right? But that’s where a lot of mistakes happen. Feed rate isn’t about how fast you can push the blade—it’s about how much material the blade is removing per tooth, a value called chip load. Let’s break that down: chip load is the amount of material each tooth on the saw blade cuts as it passes through the material. For carbon steel, a good chip load is around 0.001 to 0.003 inches per tooth; for stainless steel, it’s half that, around 0.0005 to 0.0015 inches per tooth, because stainless is harder and more abrasive. For aluminum, it can be a bit higher, around 0.002 to 0.004 inches per tooth, since aluminum is softer and chips are easier to clear.
So how do you get from chip load to feed rate? The formula is pretty straightforward, but it’s worth memorizing if you’re setting up cuts on a regular basis: Feed Rate (IPM) = Chip Load (inches per tooth) × Number of Teeth per Inch on the Blade × Blade Speed (feet per minute, FPM). Let’s test that with a common example, because numbers are easier to grasp than theory. Say you’re cutting 1045 carbon steel, the most common steel used in fabrication. You’re using a 10/14 variable-tooth blade—10 teeth per inch for thick material, 14 for thin. The blade speed for 1045 is around 150 FPM. If your desired chip load is 0.002 inches per tooth, that works out to: 0.002 × 12 teeth per inch (wait, variable blade average works here too) × 150 FPM = 3.6 IPM. That’s not a fast number by any stretch, but that’s the sweet spot for that cut. If you bump that feed rate up to 7 IPM, you’re asking each tooth to cut twice as much material, which will overheat the blade, cause premature dulling, and can even lead to blade breakage mid-cut, which is a major safety hazard in a shop.
But here’s the thing: that formula isn’t a one-size-fits-all rule. As a semi-automatic band saw supplier, I’ve seen shops use that formula, plug in the numbers, and still get bad results because they forgot to adjust for the specific job. For example, if you’re cutting thin wall pipe (under 1/4 inch thick) instead of a solid steel bar, you need to lower the feed rate. Thin wall material doesn’t have enough rigidity to support the blade’s feed, so a higher feed rate will cause the blade to vibrate, resulting in a wobbly, inaccurate cut. Conversely, if you’re cutting a solid 8-inch steel block, you can run the feed rate a bit higher than the average, because there’s enough material to keep the blade stable and the chips moving out.
Another big variable is blade type, and this is where I see a lot of new operators mix up settings. Bi-metal blades, the most common type for semi-automatic band saws, have a high-speed steel tooth that’s welded to a flexible steel back. They can handle higher feed rates than carbide-tipped blades, which are used for very hard materials like tool steel or cast iron. Carbide blades require a lower feed rate, around 0.0003 to 0.0008 inches per tooth, because carbide is brittle and can chip if it’s forced to cut too much material per tooth. I once had a customer call me in a panic, saying their new carbide blade broke after three cuts on cast iron—turns out they were using the same feed rate they used for their bi-metal blades on steel, which was way too high for the carbide teeth. It took 10 minutes to adjust their settings, and they didn’t have to replace a $150 blade that would’ve been ruined by rushing the job.
Wait, let’s also talk about what happens when feed rate is too low, because that’s the other side of the coin. Operators who are nervous about breaking blades will sometimes dial the feed way down, to the point where the blade is barely nudging the material. That might sound safe, but it causes two problems: first, the blade will rub against the material instead of cutting, generating heat that dulls the teeth just as fast as too high a feed rate. Second, low feed rates create tiny, curled chips that get stuck between the blade teeth, leading to clogging. Clogged blades don’t cut as well, and they can cause the material to heat up even more, which ruins the edge finish and can make the part inaccurate. For example, if you’re cutting a part that needs to be milled or machined next, a burnt edge from a clogged blade will add extra time to the next step, because you have to grind or sand the burnt area down before you can move on.
Now, let’s get specific to semi-automatic band saws, because their feed rate control is a bit different from manual or full automatic models. Manual band saws have a lever that you squeeze to adjust feed pressure, so feed rate is dependent on the operator’s strength and consistency. Full automatic band saws have a programmable feed rate that’s locked in for the entire cut, and they can adjust it on the fly if the material is uneven. Semi-automatic models are in between: most have a hydraulic feed system, which is what gives you that smooth, controlled advance, and a dial to set the feed speed. Some premium semi-automatic models have a digital feed rate display, so you can input numbers directly instead of guessing, while more basic models have a numbered dial. The key with semi-automatic is that you don’t have to constantly adjust the feed like you would on a manual saw, but you do have to set it correctly at the start of the cut. I always tell customers: take two minutes at the setup phase to calculate or test your feed rate, and you’ll save hours of downtime, wasted blades, and bad parts over the life of the machine.
Testing feed rate is a good practice for new jobs, especially if you’re working with a new material or a new blade. If you’re not sure what the right feed rate is, don’t jump straight to the number from the formula—start low, make a short test cut, and see how the blade performs. Look at the chips: if they’re short, broken, and dusty, that means you’re feeding too slow, the blade is rubbing. If the chips are long, stringy, and curling too tightly, that’s too fast, the blade is working too hard. The ideal chip is a long, uniform curl, about 6 to 12 inches long, that breaks evenly as it comes off the blade. If you see that, you’ve got the feed rate right.
I’ve seen this play out with a customer who makes custom motorcycle parts a few months back. They were struggling with cuts on 316 stainless steel, which is known for being gummy and hard to saw. Their old manual saw was giving them rough cuts and broken blades, so they bought a semi-automatic band saw from us, but they kept setting the feed rate too high, frustrated that they were still having issues. We walked them through the feed rate formula, adjusted their blade to a 10-tooth bi-metal blade, and set the feed rate to around 2 IPM instead of the 5 they’d been using. After that, their blade life doubled, their cuts were accurate within a thousandth of an inch, and their production time went up 20% because they weren’t replacing blades every other week. That’s the power of getting feed rate right—it’s not just a number, it’s a way to make your whole operation smoother.
Another common question I get: does feed rate matter if I’m cutting thin material, like sheet metal? Yes, it does, but the numbers change. For sheet metal under 1/8 inch thick, you want a higher blade speed (around 200 to 250 FPM) and a lower feed rate, because thin material can’t support the blade’s forward pressure. If you set the feed rate too high on thin sheet metal, the blade will “dig in” or wander, cutting at an angle instead of straight. I always recommend using a blade with more teeth per inch for thin material—18 to 24 teeth per inch—because more teeth mean each tooth is cutting less material, so you can keep the feed rate low without wasting time on the cut. For example, cutting 16-gauge steel sheet: blade speed of 220 FPM, 18 teeth per inch, chip load of 0.001 inches per tooth, that works out to 3.96 IPM. If you go higher than 4 IPM, you’ll get a wobbly cut.
There’s also a myth that harder materials need faster feed rates to get through them, which is totally backwards. The harder the material, the lower your feed rate should be. That’s because hard materials like tool steel or titanium don’t deform easily, so forcing the blade to cut too much per tooth will chip or break the teeth. For titanium, which is used in aerospace parts, the feed rate is even lower than stainless—around 0.0004 inches per tooth, so you’re looking at a feed rate of 1 to 1.5 IPM for most cuts. It seems slow, but it’s the only way to get a clean cut without damaging the material, which is non-negotiable for aerospace parts that have to meet strict quality standards.
As a semi-automatic band saw supplier, my job isn’t just to sell a machine—it’s to make sure my customers get the most out of it, and feed rate is one of the biggest levers for that. I tell every new customer: don’t treat the feed rate dial like an afterthought. Take the time to learn how it works, adjust it for your specific materials and blades, and test it on a scrap piece before you cut your actual parts. The extra two minutes at setup will save you hours of downtime, wasted material, and broken equipment down the line.
If you’re in the market for a semi-automatic band saw, or you’re looking to improve your current sawing process, we can help you work out the right feed rates for your common jobs, recommend the right blades for your materials, and answer any questions you have about setting up your machine. Contact our team to discuss your specific needs and find the right solution for your shop.
Vertical Band Saw Series References
- Kalpakjian, S., & Schmid, S. R. (2014). Manufacturing Processes for Engineering Materials. Pearson Education.
- ASME B107.1-2018, Safety Standard for Band Saws. American Society of Mechanical Engineers.
- Saw Blade Technical Handbook. (2021). Leitz Tools North America.
- Metalworking Band Sawing Best Practices. (2020). American Fabricators & Manufacturers Association (FMA).
Shanghai Loginfly Sawing Technology Co., Ltd.
As one of the most professional semi-automatic band saw manufacturers and suppliers in China, our products have good reputation in the market. We warmly welcome you to wholesale premium semi-automatic band saw from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: Room 506 NO.655 Yinxiang Road,Nanxiangtown,Jiading District, Shanghai.China
E-mail: sales01@loginfly.com
WebSite: https://www.loginflysaws.com/
