When I first started out as a cryogenic ball valve supplier, I quickly learned that even the highest-quality valve won’t perform as intended if it’s installed wrong. I’ve seen it too many times: a client purchases our top-of-the-line cryogenic valve, skips the proper installation steps, and ends up with leaks, pressure drops, or even a system shutdown that costs them weeks of production. That’s why I want to share the practical, science-backed installation guidelines we’ve refined over years of working with cryogenic systems—steps that aren’t just industry standards, but lessons we’ve helped dozens of clients implement to keep their cryogenic processes running smoothly. Cryogenic Ball Valve
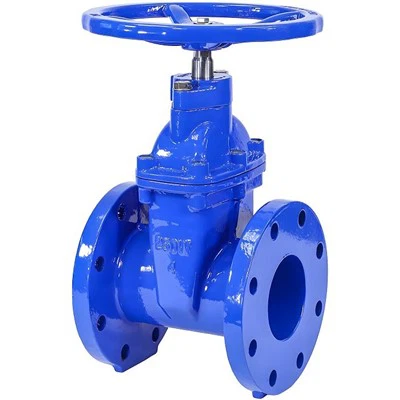
First, let’s ground this in what makes cryogenic valves different. Unlike standard industrial valves, cryogenic ball valves are designed to handle temperatures below -150°C, often dropping to -196°C for liquefied nitrogen, oxygen, or argon. These extreme colds cause metal to contract, seal materials to become brittle, and moisture to turn to ice—all of which can ruin a valve’s performance if installation doesn’t account for them. I always tell my clients: installation for cryogenic systems isn’t just bolting a valve between two pipes; it’s about mitigating the unique stresses of cryogenic service before they even start.
The first step, before you ever lift a valve, is pre-installation inspection and preparation. I’ve had a few clients skip this part because they “trusted the brand,” but inspection catches issues that happen during shipping. When our valves leave our facility, they’re sealed with protective caps on the ports to keep debris out, but those caps are easy to forget to remove. Here’s how we walk clients through inspection: first, visually check the valve body for dents or scratches—even a tiny nick on the valve’s seat can create a leak path when the system cools down. Next, test the actuator (if your valve has one) to make sure the ball turns smoothly; a stiff actuator pre-installation will be impossible to operate once it’s mounted to the pipe. Most importantly, verify the valve’s material matches your system. Cryogenic valves use specific materials like 316L stainless steel or low-carbon alloy steel to avoid embrittlement. I once had a client try to use a standard carbon steel valve because it was cheaper, and within three months, the valve cracked at -180°C. That’s a mistake no supplier wants a client to make, so we always stress material verification in pre-install checks.
Next, pipe preparation is critical. Cryogenic systems are precision environments, so any misalignment in the pipe flanges will cause stress on the valve’s body when you bolt it on. I recommend having a qualified pipe fitter check the flange faces for flatness first. Even a 0.5mm deviation in flange flatness can lead to uneven gasket compression, which will leak under cryogenic conditions. You also need to clean the pipes thoroughly—no oil, grease, or metal shavings allowed. Oil might seem harmless, but at cryogenic temperatures, it can polymerize and solidify, clogging the valve’s seat and causing it to bind. We always suggest using a non-solvent-based cleaning method (like compressed dry nitrogen) to blow out any debris, and then capping the pipe ends right up until you’re ready to connect them to the valve. That prevents any new dust or dirt from getting in, which is a common late-stage mistake.
When it’s time to mount the valve, pipe alignment is non-negotiable. Cryogenic ball valves are designed to support the weight of the line, but if the pipes pull the valve at an angle, the body will flex when it cools, leading to seal failure. I advise using a pipe alignment tool to make sure the centerlines of the inlet and outlet pipes are perfectly aligned with the valve’s port. If there’s any misalignment, adjust the pipe supports before bolting the valve—don’t force the bolts. For flanged valves, use a gasket that’s compatible with cryogenic service. Most of our clients use PTFE (for lower pressures) or graphite-filled gaskets, but I always recommend checking the valve’s datasheet to confirm. Another tip: apply a thin layer of cryogenic-compatible anti-seize compound to the bolt threads before tightening. This makes future maintenance (like removing the valve) much easier, and it prevents bolts from seizing up when cold. When tightening the flange bolts, use a crisscross pattern to ensure even compression—tighten each bolt a little at a time, going around the flange, until all are at the manufacturer’s specified torque. Over-tightening can crush the gasket, leading to leaks, while under-tightening will leave gaps. I usually give clients a torque chart for each valve size, since a 2-inch valve needs a different torque than an 8-inch one.
Then comes a step that many first-timers overlook: insulation and cold box preparation. Cryogenic valves need insulation to minimize heat ingress, which causes liquefied gases to vaporize, leading to pressure spikes. But you can’t just wrap the valve in insulation right away. You need to make sure there’s a small gap (usually 10-15mm) around the valve body and actuator for insulation. If you cover the valve’s bolt connections or actuator with insulation, you won’t be able to inspect for leaks during operation. For buried or submerged cryogenic systems, you also need to install a secondary heat shield around the valve to prevent ground moisture from freezing on the valve body. I’ve seen insulation that was too tight cause a problem called “cold trapping”—moisture that gets stuck between the valve and insulation freezes, expanding and cracking the valve’s body. So always leave that small air gap, and use a closed-cell insulation material (like polyurethane foam) that doesn’t absorb moisture.
Once the valve is installed, there’s a critical pressure test before putting the system into full service. Don’t jump straight to liquid nitrogen—start with a dry gas test, usually using dry nitrogen at 1.5 times the system’s operating pressure. This lets you check for leaks without the extreme cold that would hide small seal issues. Pressurize the system, hold it for at least 30 minutes, and monitor the pressure gauge. If the pressure drops more than 5%, you have a leak. To find where, use a soapy water solution (but not the kind with oil) on the flange connections and valve body—bubbles will form at the leak point. Once the dry test passes, do a cold shock test. This is where you introduce a small amount of cold liquid (like liquid nitrogen) into the system gradually, starting with a flow rate that’s less than 10% of the valve’s maximum. Let the system cool for 2-3 hours, then check for any leaks or unusual sounds from the valve. This step ensures the valve’s seals and components have time to contract slowly, avoiding thermal shock that could crack the valve.
After all these steps, ongoing maintenance is part of proper installation too. I always tell clients that a cryogenic valve’s life depends on how you care for it after installation. For example, you shouldn’t leave the valve in the half-open position for long periods—this causes the ball to rub against the seat, leading to wear. We recommend exercising the valve (turning the ball fully open and fully closed) every 30 days, even if it’s not in use. This keeps the seals lubricated and prevents the ball from sticking due to cold contraction. Also, check the insulation annually for gaps or damage, since water or air getting into insulation can ruin its effectiveness.
Let me circle back to why this matters for you, as a cryogenic system operator. I’ve had clients come to me after a failed installation, and the cost of replacing a valve, repairing the pipe, and lost production is often 10 times the cost of following these guidelines. The goal here isn’t just to install a valve—it’s to make sure it performs consistently for years, handling the extreme cold, pressure, and vibration of your cryogenic system.
If you’re planning a cryogenic system upgrade or need a reliable cryogenic ball valve, I’m here to walk you through every step of the process, from selecting the right valve to troubleshooting any installation issues. Don’t let a simple installation mistake derail your operations—reach out to start a conversation about your specific needs.
Check Valve References
- ASME B31.3 Process Piping Code, American Society of Mechanical Engineers
- Cryogenic Valve Design and Installation Guide, Compressed Gas Association
- Materials for Cryogenic Service, International Organization for Standardization (ISO) 15547
- Industrial Cryogenic Valve Installation Best Practices, Cryogenic Society of America
Wuxi PYNOS Flow-tech Co., Ltd.
As one of the leading cryogenic ball valve manufacturers and suppliers in China, we offer a wide range of products with superior quality. We warmly welcome you to buy high quality cryogenic ball valve made in China here from our factory. We also accept customized orders.
Address: Sales Center: 7th Floor, No.19 Qingyuan RD, Wuxi City, Jiangsu Prov., China
E-mail: Info@pynosvalve.com
WebSite: https://www.pynosvalves.com/
